Medical Grade Film is a pretty vital part of the healthcare world. Its toughness and flexibility make it perfect for all sorts of medical uses. Not only does it help protect sensitive stuff, but it also boosts how well medical devices work. Lots of big names like 3M and DuPont rely on Medical Grade Film for things like wound care and surgeries. It acts as a sterile barrier but still lets the skin breathe—big plus for patient comfort and healing. But here’s the thing: not all Medical Grade Films are created equal. Picking the right one can honestly feel a bit overwhelming. Sometimes, the choices can leave you scratching your head and wanting some expert advice. In a busy setting, mistakes happen—no big surprise. That’s why it’s so important to really understand what you need and what each type offers. Getting a handle on the benefits can help you make smarter decisions and get the most out of Medical Grade Film in whatever situation you’re dealing with.
Medical grade film is specifically designed for use in healthcare environments. This type of film must meet strict regulatory standards. It is made to be durable, sterile, and safe for patient care. According to a report by ResearchAndMarkets, the global medical films market is expected to grow by over 6% from 2021 to 2026. This highlights the importance of understanding its characteristics.
The primary characteristics of medical grade film include high clarity and resistance to moisture. Such films ensure that healthcare providers can visualize wounds or injuries effectively. They are often used for surgical draping and medical packaging. Some films may lack flexibility, which can limit their applications in dynamic environments. Moreover, while many films possess barrier properties, not all are equally effective against various contaminants.
These limitations prompt ongoing research. Improving the mechanical properties of these films can enhance their usability. Industry experts note that integrating advanced materials can result in better performance. A balance between cost and functionality remains a challenge in the development of medical grade films.
Medical grade films are essential in healthcare settings. They serve various purposes, from sterile packaging to wound care and more. Common materials used in these films include polyurethane, polyvinyl chloride (PVC), and polyethylene. Each material offers distinct properties suited for different applications. For example, polyurethane films are known for their durability and flexibility. They provide excellent moisture vapor transmission, crucial for wound healing.
Studies indicate that polyurethane films contribute to a 36% increase in healing rates. This highlights their importance in medical applications. Polyvinyl chloride (PVC) is another widely used material. It is often selected for its clarity and ease of sterilization. However, concerns over plasticizers in PVC have surfaced. While effective, there is a need for alternatives that address potential health risks.
Polyethylene also finds its place in medical films, especially for packaging. It offers good chemical resistance and is often used for sterile barrier systems. This material can enhance product safety. However, it may not provide the same level of breathability as polyurethane. Each choice comes with its own set of trade-offs. As the industry evolves, continuous improvement in material safety and efficacy remains a challenge.
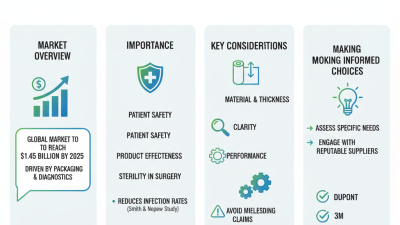
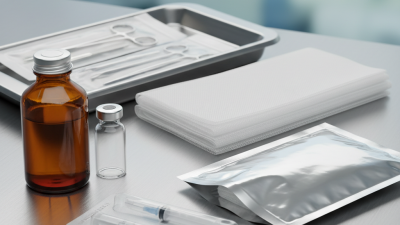
Medical grade film plays a vital role in healthcare settings. It is primarily used for packaging medical devices and supplies. This type of film ensures the sterility and safety of products before use. According to a report by Grand View Research, the global medical packaging market is expected to reach $37 billion by 2026, reflecting the increasing need for effective medical solutions.
In hospitals, medical grade film is often used in wound care. It provides a barrier against moisture and bacteria. A study published in the Journal of Wound Care showed that high-quality films can reduce infection rates by 30%. This is crucial when treating post-operative patients. The film’s transparency allows for easy monitoring of the healing process without removal.
Another application is in the production of sterile pouches. These pouches are essential for storing instruments. The effectiveness of these pouches relies on the film’s durability and seal integrity. However, improper sealing can lead to contamination. Healthcare workers need to be aware of this risk. Awareness and training can enhance the efficacy of these medical applications, ensuring better patient outcomes.
Medical grade film is essential in various medical applications. It is specially designed to meet strict health standards. According to the International Organization for Standardization (ISO), medical films must comply with specific regulations to ensure safety and efficacy. These films are commonly used for packaging sterile medical devices and in wound care.
One of the key benefits is their barrier protection. Medical grade films can protect against moisture and bacteria. A study published in the Journal of Medical Products found that films with high moisture vapor transmission rates can compromise sterile contents. Therefore, using medical grade films reduces contamination risks significantly. They also allow for easy visualization of the contents, which is crucial in medical settings.
However, there are challenges. The cost of medical grade films can be higher than conventional materials. Some facilities may hesitate to adopt them due to budget constraints. There is also a need for ongoing testing to ensure performance standards are consistently met. As the medical field evolves, more research is needed to assess the long-term benefits and potential drawbacks of using these specialized films in diverse applications.
This bar chart illustrates the benefits of using medical grade film in medical applications. It highlights key attributes such as barrier protection, biocompatibility, durability, flexibility, and clarity, showcasing their respective importance in percentage terms.
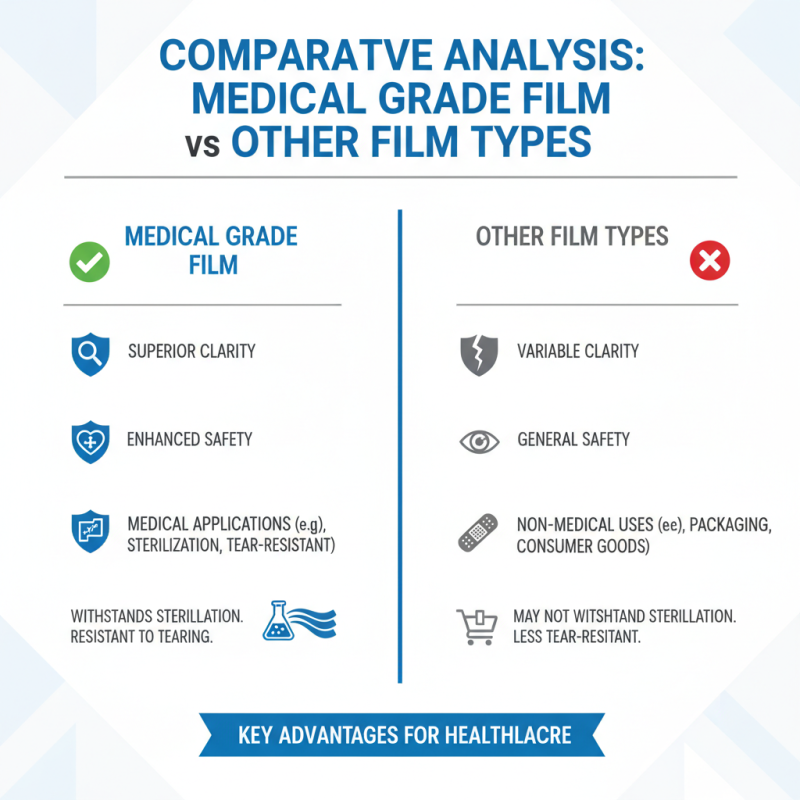
When comparing medical grade film to other film types, key differences emerge. Medical grade film offers superior clarity and safety. Its design specifically caters to medical applications. This film type withstands sterilization processes and is resistant to tearing.
In contrast, standard films may lack these features. Their durability is often lower, which can lead to issues in clinical settings. Using non-medical films in healthcare might compromise patient safety. Therefore, consideration of material is crucial.
**Tips:** Always choose films that meet medical standards. Check for certifications. Assess the specific needs of your application. This helps avoid potential complications.
Using the right film type improves outcomes significantly. Yet, not everyone realizes the importance of quality. Sometimes, cost-cutting leads to regrettable choices. Reflect on the long-term impacts of using inferior films in medical environments.
Medical grade films are crucial in healthcare settings. To ensure safety and effectiveness, these films must meet specific
regulatory standards. Regulatory bodies define these standards based on clinical needs. They assess materials, manufacturing processes, and end-use applications. Compliance is not just a guideline; it affects patient safety.
Understanding these standards is vital for manufacturers. It is not always straightforward. Companies may face challenges in meeting all requirements. Testing procedures can be complex and time-consuming. Each film type has unique attributes that must match the intended use. For instance, sterilization compatibility is often mandatory. If a film cannot withstand various sterilization processes, it may pose risks.
Failing to adhere to these standards can lead to severe consequences. Not only can it affect product integrity, but it also impacts patient care. The nuances of regulatory compliance must be acknowledged. Continuous reflection on manufacturing practices is necessary. Improving processes can lead to better outcomes in healthcare applications. This commitment to quality ensures that medical professionals have reliable tools for patient care.
The medical grade film sector is evolving rapidly. Innovations focus on greater functionality and improved safety. Emerging technologies enhance the biocompatibility of these films. This means better integration with biological tissues. Researchers are exploring new materials that are more durable yet flexible. These advancements could significantly reduce infection risks during medical procedures.
Sustainability is also a growing concern. Many companies aim to produce eco-friendly films that minimize environmental impact. These films may offer similar performance to traditional options but with reduced waste. There is a push to develop biodegradable alternatives. However, balancing performance and environmental responsibility remains a challenge.
As the healthcare landscape shifts, adaptability becomes crucial. Films must cater to diverse applications, from wound care to surgical drapes. User feedback often drives enhancements, highlighting the need for continuous improvement. The aim is to create films that not only meet current needs but also anticipate future demands. Embracing innovation while considering practicality is essential in this field.
: Medical grade film is designed for healthcare use. It meets strict regulatory standards for safety and durability.
Key characteristics include high clarity, moisture resistance, and durability. They help visualize wounds effectively in care settings.
Regulatory standards ensure safety and effectiveness. Compliance affects material choice, manufacturing, and patient safety.
Manufacturers often struggle with complex testing and compliance requirements. Each film type has unique regulatory attributes.
Many medical films lack flexibility. This can limit their use in dynamic healthcare environments.
Continuous improvement can enhance film properties. Reflecting on practices is crucial for better healthcare outcomes.
While many films possess barrier properties, their effectiveness varies. Not all films protect equally against contaminants.
Failing to meet standards can compromise product integrity and patient care. Serious consequences may arise from non-compliance.
Medical Grade Film is a specialized type of film designed for use in healthcare settings, characterized by its biocompatibility, durability, and ability to maintain sterility. Common materials used in medical grade films include polyethylene, polyvinyl chloride, and polyurethane, each selected for specific applications like wound care, surgical drapes, and packaging for medical devices. The benefits of using Medical Grade Film are significant, as it helps protect against contamination, enhances patient safety, and ensures compliance with strict regulatory standards.
In addition, a comparative analysis reveals that Medical Grade Film often outperforms other types of films in terms of performance and safety, making it essential for various medical applications. As innovations continue to emerge, the future of Medical Grade Film technology promises improved functionality and efficiency, highlighting its critical role in the advancement of healthcare products and practices.