Medical packaging materials really play a crucial role in healthcare — I mean, they’re kinda the unsung heroes. These materials are what keep medical products safe and intact, preventing any contamination, damage, or breakdown during shipping and storage. It’s one of those things you don’t always think about, but they’re super important.
When it comes to types, you’ve got plastics, glass, and metals — each one kind of has its own thing going on. For instance, plastics are pretty lightweight, which is great, but they might not cut it if you need something sterilized at high temperatures. Glass, on the other hand, is reliable and more resistant to certain stuff, but it can also be heavy and fragile as hell. Companies like Medline and DuPont are always pushing the envelope, coming up with new ideas and better solutions.
Honestly, the importance of medical packaging material can’t be overstated — it directly affects patient safety and how well the products work. Still, folks in the industry gotta keep asking themselves tough questions: Are their packaging choices sustainable? Are they user-friendly? These are the little details that really matter, and they need some real thought and care.
Definition of Medical Packaging Material
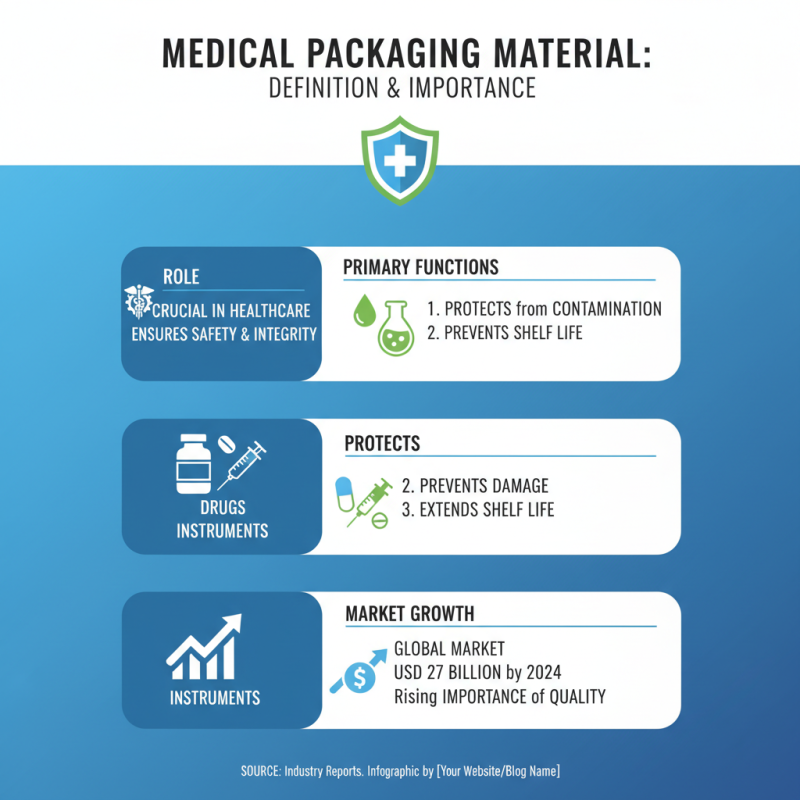
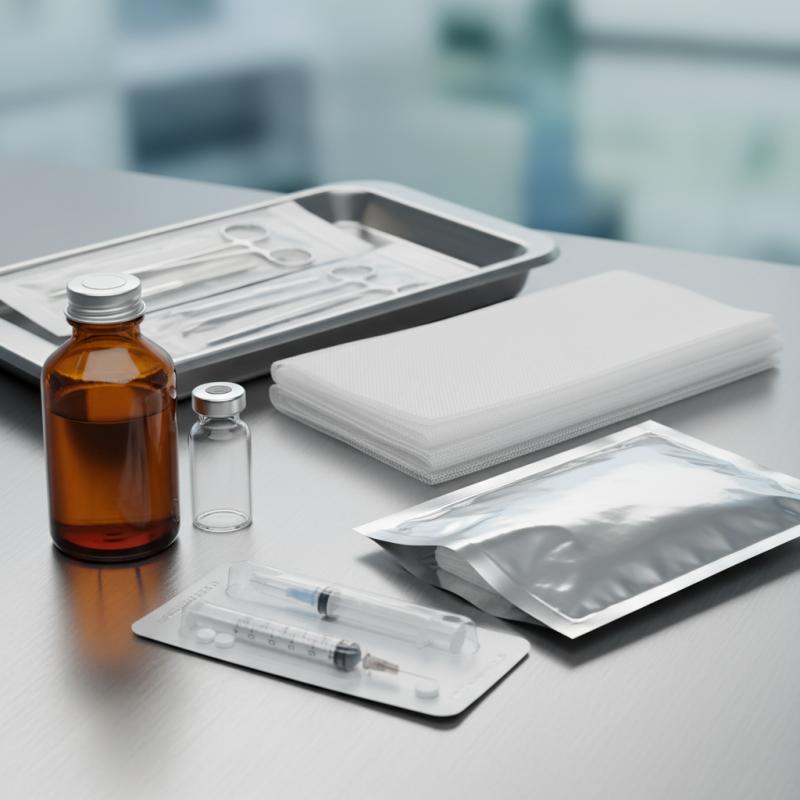
Medical packaging material plays a crucial role in the healthcare industry. It ensures the safety and integrity of medical products. This packaging safeguards drugs, instruments, and devices from contamination and damage. It also extends shelf life. According to industry reports, the global medical packaging market is projected to reach USD 27 billion by 2024. This shows the rising importance of quality in medical packaging.
These materials come in various forms, such as pouches, blisters, and cartons. They are designed to meet strict regulatory standards. This ensures that the products remain sterile. A study from the Pharmaceutical Care Network found that improper packaging can lead to a 15% increase in product spoilage. Such statistics highlight the need for ongoing improvements in packaging processes.
**Tip:** Always choose packaging that balances protection and sustainability. Look for materials that are recyclable or biodegradable. This helps to reduce environmental impact while maintaining safety standards. Reflect on the current practices used in your facility. Are they meeting safety requirements? Are there innovations that could enhance protection? These questions are essential for continuous improvement in medical packaging.
Types of Medical Packaging Materials Used in Healthcare
Medical packaging materials play a crucial role in healthcare.
They ensure the safety and efficacy of medical products. Various materials are used to meet different needs in the medical field.
Plastic is commonly used for packaging. It is lightweight and flexible.
Another popular option is glass.
Glass is often preferred for its chemical resistance and ability to maintain sterility. However, it can be heavier and more fragile.
Paper and cardboard are also important, especially for packaging disposables.
They are eco-friendly and easily customizable.
Despite the variety, some challenges remain. Not all materials provide the same level of protection.
Sometimes, the packaging fails to maintain sterility. In other cases, the materials are not compatible with the products stored inside.
This can lead to contamination or deterioration. Evaluating the choice of materials is essential in ensuring patient safety and product effectiveness.
Key Properties of Effective Medical Packaging
Medical packaging material plays a crucial role in the healthcare industry. Effective packaging must protect medical products from contamination and damage. According to a report by ResearchAndMarkets, the global medical packaging market is expected to reach $202 billion by 2027. This growth highlights the increasing importance of choosing the right packaging.
Key properties of effective medical packaging include barrier protection, durability, and compatibility. Barrier properties prevent moisture, oxygen, and light from compromising the product. For instance, materials like flexible films often maintain a sterility rate above 99% when properly sealed, as reported by PackagingInsights. However, not all materials achieve this level of effectiveness consistently.
Durability ensures that packages withstand shipping and handling. According to an industry study, nearly 40% of products are damaged during transit due to inadequate packaging. This statistic raises concerns about the reliability of many packaging solutions. Moreover, compatibility with the medical product itself is essential. Incorrect materials can lead to chemical reactions or alter product efficacy. These factors must be critically analyzed to ensure patient safety and preserve product integrity.
Importance of Key Properties in Medical Packaging Materials
This chart illustrates the importance level of various key properties of medical packaging materials, highlighting how critical barrier properties and shelf life are for maintaining product integrity and safety.
Regulatory Standards for Medical Packaging
Regulatory standards for medical packaging are essential for ensuring safety and efficacy. These standards guide the design, materials, and performance of packaging used in healthcare. According to the International Organization for Standardization (ISO), specific standards, such as ISO 11607, outline requirements for sterile barrier systems. These guidelines help maintain the integrity of medical devices and pharmaceuticals throughout their lifecycle.
Compliance with these regulations is crucial. A report from MarketsandMarkets indicates that the medical packaging market will reach $27.4 billion by 2025, emphasizing the demand for high-quality materials. However, many companies struggle to keep pace with evolving regulations. Some fail to adopt adequate testing methods. Others overlook necessary documentation. These missteps can lead to costly recalls and damage to reputations.
Inadequate packaging can compromise product safety. A survey by the Healthcare Packaging Association found that 42% of respondents noted packaging failures that resulted in product damage. This highlights the need for stringent adherence to regulations. The industry must focus on continuous improvement and invest in advanced technologies. Embracing innovation is necessary to meet regulatory challenges effectively.
The Role of Medical Packaging in Product Safety
Medical packaging plays a crucial role in ensuring product safety in the healthcare sector. With an estimated 2.5 million injuries related to improper packaging every year, the stakes are high. Efficient packaging protects medical products from contamination and damage. It acts as a barrier against environmental factors, thereby safeguarding the integrity of the materials inside.
The design and material selection in medical packaging are vital. According to a recent industry report, around 30% of recalls stem from packaging failures. This highlights the need for robust packaging systems that can endure transportation and storage conditions. Material durability, ease of use, and visibility are essential factors. Hospitals often face challenges with complex packaging that may lead to user errors. Ensuring intuitive designs can help mitigate risks.
Regulations also demand a focus on safety. The FDA requires stringent tests for packaging materials. These tests cover everything from permeability to compatibility with the products inside. However, not all manufacturers adhere to these standards. This inconsistency can lead to vulnerabilities in the supply chain. The importance of thorough oversight cannot be stressed enough, as failures can have dire consequences for patient safety.
Impact of Medical Packaging on Shelf Life and Efficacy
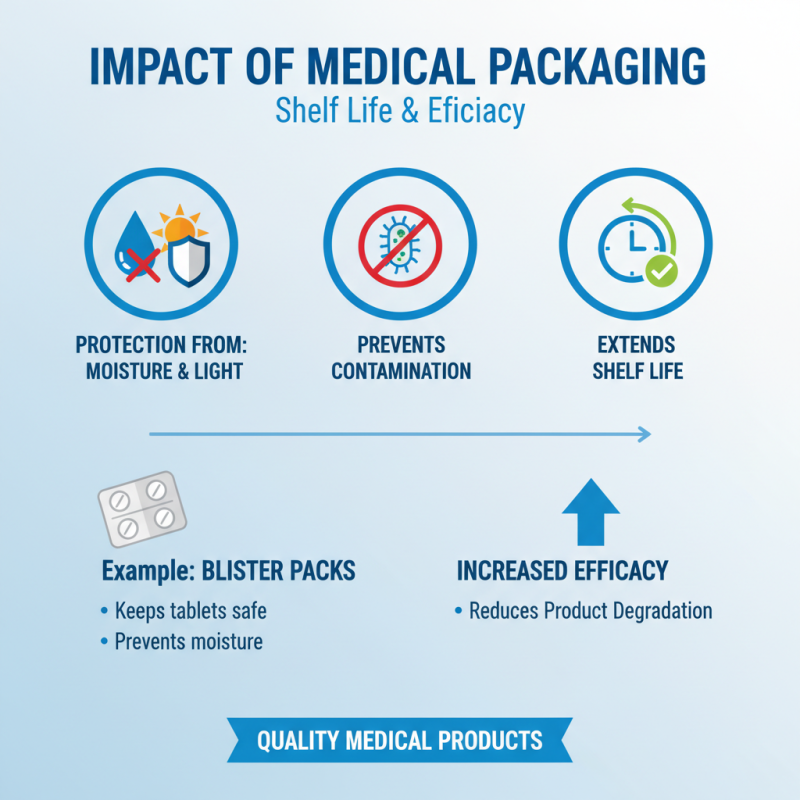
Medical packaging material plays a crucial role in extending the shelf life and efficacy of medical products. Proper packaging protects against environmental factors such as moisture, light, and contamination. Effective materials can significantly reduce the risk of product degradation. For instance, blister packs can keep tablets safe and prevent moisture from compromising their quality.
The impact of poor packaging can be severe. Some medical products may spoil prematurely if not sealed correctly. The effectiveness of a medication may diminish due to improper storage. Packaging must ensure that items remain sterile and intact until they reach the end-user. However, not all manufacturers prioritize packaging equally, leading to inconsistencies in product safety.
Beyond protection, packaging also supports user confidence. Clear labeling and design improve accessibility for healthcare professionals and patients. When packaging fails to communicate vital information effectively, it can lead to improper usage. Reflecting on these aspects prompts a critical examination of current practices in medical packaging.
Emerging Trends in Medical Packaging Technology
The medical packaging industry is evolving rapidly.
New technologies are emerging to meet the needs of healthcare. Innovations focus on improving safety and efficiency.
For instance, smart packaging utilizes sensors to monitor the condition of medical products.
These sensors track temperature and humidity levels, ensuring that products remain within safe limits.
Another trend is biocompatible materials.
These materials are designed to minimize allergic reactions or adverse effects on patients. By using
sustainable resources, manufacturers aim to reduce environmental impact.
However, the transition to these materials can be challenging. They often require new manufacturing processes that may not yet be fully tested.
Challenges remain in balancing cost and quality.
High-quality materials can be expensive, making it difficult for smaller companies to compete.
Regulatory hurdles also add layers of complexity. Companies must navigate these while keeping an eye on innovation.
The landscape is dynamic, necessitating both creativity and caution in implementation.
Exploring the Impact of Coated Cellulose Film on Sustainable Packaging: Insights from the Latest Industry Reports
The increasing demand for sustainable packaging solutions highlights the pivotal role of innovative materials like coated cellulose film. This premium packaging option, derived from natural cellulose, not only adheres to stringent industry standards like ISO9001 and ISO14001 but also complies with EU food contact regulations. Engineered for high-performance applications, coated cellulose film showcases exceptional heat-sealability and significantly enhanced barrier properties, effectively protecting products from moisture and oxygen. This capability is crucial for industries such as food packaging, where preserving freshness is paramount.
In addition to its functional benefits, coated cellulose film offers superior printability that allows for vibrant branding and consumer engagement. Its versatility makes it an ideal choice for a variety of applications, including food items like dried fruits and confectionery, as well as tea and coffee pouches and luxury gift packaging. As manufacturers globally seek to replace traditional plastics with sustainable alternatives, coated cellulose film stands out as a reliable and environmentally friendly option, supporting the industry's transition towards more responsible packaging practices while meeting the rigorous demands of both technical performance and environmental sustainability.
FAQS
: It protects medical products from contamination and damage, ensuring safety and integrity.
Proper packaging can extend shelf life by safeguarding products from external factors.
Common forms include pouches, blisters, and cartons designed to meet strict standards.
Improper packaging can lead to a 15% increase in product spoilage, affecting safety.
Key properties include barrier protection, durability, and compatibility with products.
It prevents moisture, oxygen, and light from compromising the product quality.
Nearly 40% of products get damaged in transit due to inadequate packaging.
Incorrect materials can cause chemical reactions or alter effectiveness, risking patient safety.
Reflect on current practices and seek innovations that enhance protection and safety.
Yes, look for recyclable or biodegradable materials to reduce environmental impact.
Conclusion
Medical Packaging Material plays a crucial role in the healthcare industry, ensuring the safe and effective delivery of medical products. It encompasses various types of materials designed to protect and preserve medical devices and pharmaceuticals while maintaining sterility. Key properties of effective medical packaging include barrier protection, compatibility with the contents, and ease of use. Additionally, compliance with regulatory standards is essential for ensuring product safety and efficacy.
The importance of Medical Packaging Material also extends to its impact on the shelf life and performance of medical products. Advances in packaging technology are continually emerging, focusing on enhancing safety and convenience for healthcare providers and patients alike. By understanding the significance of Medical Packaging Material, stakeholders can truly appreciate its vital role in maintaining the integrity of medical products throughout their lifecycle.